
Why Custom Grades and Third-Party Testing Delay Steel Plates from China
Why Custom Grades and Third-Party Testing Delay Steel Plates from China
Steel plate lead time from China can stretch beyond your project schedule when custom grades require mill approval, dedicated production runs, or additional testing. Third-party inspection adds another scheduling dependency, particularly when sampling, laboratory availability, and document review must align before shipment. For project managers, these delays can disrupt fabrication milestones and complicate procurement planning. Understanding where extra time enters the process helps you set realistic delivery dates, define testing requirements early, and coordinate supplier and inspector schedules before production begins.
The key distinction is between material that exists and material that is approved for your project. A plate may already be rolled, yet remain unavailable for shipment because its traceability records, test results, or inspection release are incomplete. Treating those two states as equivalent is a common source of unrealistic delivery commitments.
A custom grade changes the production route, not just the description
“Custom” can mean a non-stock grade, a tighter chemical composition, an unusual thickness, a specified delivery condition, or additional toughness requirements. These requests do not create the same scheduling burden. Cutting a stocked plate to a different outline is fundamentally different from producing steel with restricted chemistry and a prescribed heat-treatment route.
Before accepting an order, the mill may need to confirm whether the requested combination is achievable on its equipment. Thickness, strength, impact properties, flatness, and delivery condition interact. A grade designation alone does not establish that every thickness or supplementary requirement is available through the same production route.
Where new production is necessary, the order must fit steelmaking, rolling, and potentially heat-treatment schedules. A small tonnage does not automatically receive a short lead time: it may need to join a compatible production campaign. Conversely, a larger quantity of standard stock can sometimes be prepared sooner than a small custom batch.
Ask the supplier to distinguish between confirmed stock, material already scheduled for production, and a proposed mill order awaiting acceptance. Each carries a different level of delivery certainty. A quotation based on a possible production slot should not be treated as a firm mill commitment.
Equivalent grades need engineering approval
When delivery pressure rises, substituting an available grade can look attractive. However, similar strength values do not prove interchangeability. Chemistry limits, impact-test conditions, weldability considerations, thickness tolerances, and delivery condition may differ between specifications. Any substitution should receive written approval from the responsible engineer before procurement proceeds.
For abrasion-related applications, a listing such as Wear-resistant Plate-(1)-(1) is a starting point for technical discussion, not confirmation that a particular grade is in stock or suitable for a welded structure. Confirm the required hardness range, thickness, processing route, and any toughness requirements before comparing delivery offers.
Third-party testing creates dependencies that cannot all run in parallel
Inspection is often described as a final visit before loading. That is only one possible arrangement. If an independent inspector must witness sample selection, verify identification, or attend a specified test, inspection activities begin earlier. Booking the inspector after production finishes can therefore be too late.
A typical dependency chain is production completion, plate identification, witnessed sampling where required, specimen preparation, laboratory testing, report review, and shipment release. Some tasks can overlap; others cannot. The laboratory cannot test a specimen that has not been prepared, and the buyer cannot approve a report that has not been issued.
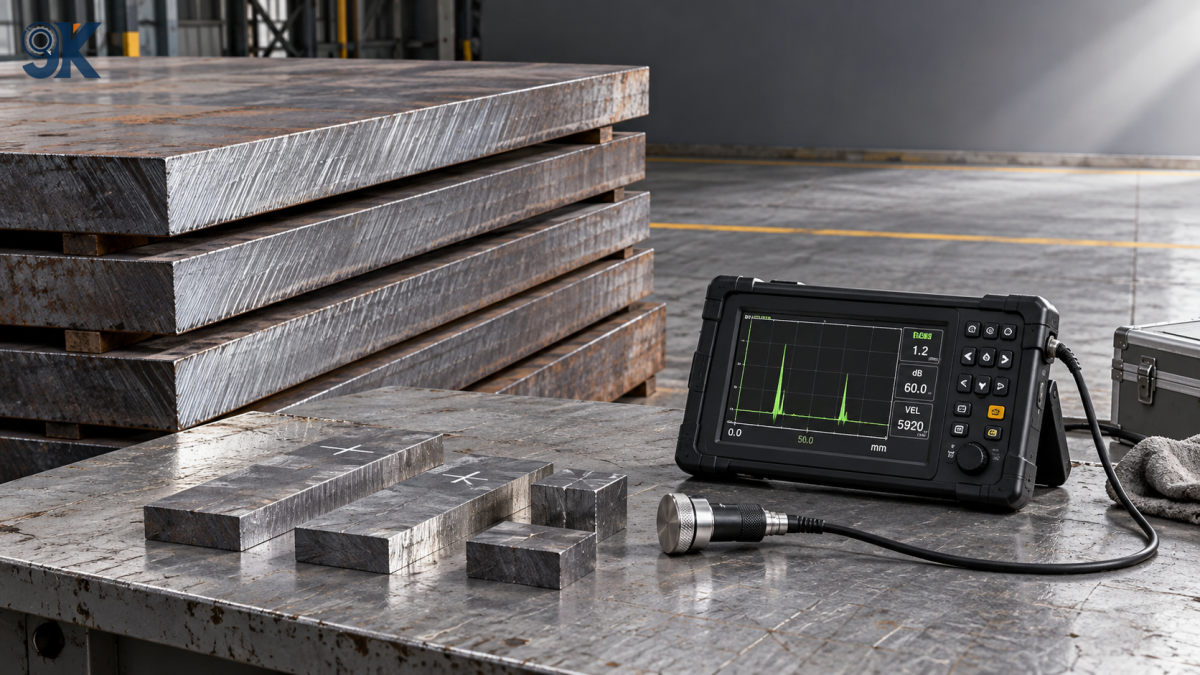
The inspection and test plan should distinguish a hold point, beyond which work cannot proceed without the specified authorization, from a witness point, where attendance and any permission to proceed depend on the agreed procedure. These terms should be defined in the contract rather than left to assumption. Otherwise, a missed visit can become a production stoppage.
Independent inspection, independent laboratory testing, and mill certification are also different services. A dimensional inspection does not establish mechanical properties. A mill test certificate does not automatically satisfy a requirement for independently witnessed testing. The purchase order should identify which evidence is required and who has authority to accept it.
Testing scope matters more than the number of tests
A short request such as “third-party testing required” leaves too much unresolved. The testing method, sampling frequency, specimen location, acceptance criteria, and reporting requirements all affect preparation and turnaround. Additional tests become especially disruptive when requested after the plates have been cut, packed, or moved away from the mill.
- Mechanical tests: Confirm which tensile and impact tests apply, including specimen orientation, test temperature, and grouping by heat or batch under the governing specification.
- Hardness checks: Define the method, measurement locations, and acceptance range where relevant. A hardness reading alone does not replace other specified properties.
- Ultrasonic examination: State the applicable standard, acceptance level, coverage, and reporting requirements. “UT passed” is not a complete acceptance criterion.
- Chemical verification: Agree on the analytical method and reporting scope. Portable identification methods may not establish every element needed for acceptance.
Destructive testing also requires enough material for suitable specimens. If test allowances are not included in the cutting plan, obtaining samples can consume usable plate or require a revised allocation. Confirm sampling arrangements before nesting production parts, especially for small-batch orders with little spare material.
Do not assume a failed result can simply be replaced by another test. Retesting must follow the applicable specification and agreed procedure. The schedule should allow for investigation, permitted retesting, or replacement material without treating any of those outcomes as guaranteed.
Document approval can become the final bottleneck
A plate can meet physical requirements and still be held because the evidence does not connect cleanly to the shipment. Heat numbers, plate identifiers, inspection records, test reports, and packing lists need a consistent traceability chain. Cutting and deep processing make that chain harder to maintain unless identification transfer is planned.
Request a sample document package before production. Agree on required fields, language, report format, signatures, and any project-specific document references. Where a particular inspection document type is specified, confirm exactly what validation it requires; generic promises of a “certificate” are insufficient.
Buyer-side review needs a deadline too. If technical queries move between procurement, engineering, the inspector, and the end user without a named decision-maker, completed material may wait while vessel cutoffs pass. Assign one owner for consolidating comments and one authority for shipment release.
Build the delivery plan around release gates
Instead of requesting one overall delivery promise, ask for a milestone schedule with dependencies. It should show when the specification freezes, when the mill accepts the order, when material becomes available for sampling, when reports are expected, and when the cargo can move to port.
Separate ex-mill readiness, port delivery, vessel departure, and arrival at the fabrication site. “Delivery in six weeks,” for example, is ambiguous unless the starting event and destination milestone are defined. Use the agreed Incoterms rule and named place, while documenting the operational schedule separately.
Contingency should sit around uncertain activities, not appear as an unexplained allowance at the end. A provisional rolling slot, a specialist laboratory booking, and buyer approval each need their own visibility. This makes recovery decisions possible before a missed milestone affects fabrication.
Reduce avoidable delay without weakening acceptance
The most effective acceleration is usually earlier coordination. Freeze safety-critical requirements first, resolve permissible alternatives with engineering, reserve inspection capacity, and review documents progressively. For mixed orders, consider releasing compliant stock separately from custom plates if traceability, freight cost, and fabrication sequencing justify it. Partial shipment is useful only when the receiving team can actually use the material.
Shandong Jiukai Metal Materials Co., Ltd. is based in Shandong and focuses on steel pipe services for machinery manufacturers, combining custom production, deep processing, warehousing, logistics, and export clearance. For a wider project package that includes plates, confirm the plate-producing mill, supply scope, and inspection responsibilities separately. Integrated coordination helps manage handoffs, but does not remove mill or laboratory constraints.
Jiukai’s shipping options through Tianjin, Qingdao, and Rizhao provide alternatives to evaluate against cargo readiness and destination service. FCL, LCL, or bulk shipment should be selected around plate dimensions, handling requirements, shipment volume, and available sailings—not simply the nearest port or lowest quoted freight.
Before committing to a fabrication date, obtain three things: a technically accepted material specification, a confirmed inspection plan, and a milestone schedule identifying who releases each stage. Steel plate lead time from China becomes more manageable when production completion is treated as one milestone—not proof that the order is ready to ship.
Latest News
- How do iron ore prices affect steel pipe price trends?
- How do tariffs affect square tube export markets?
- How steel pipe price trends affect inventory valuation
- Steel pipe price forecast for 2026 amid changing raw material costs
- Square Tube Export News: What Buyers Should Watch in Freight and Supply
- What new trade investigations mean for steel pipe exports
Send Us A Message

